
Output control judges performance by measuring results, not by supervising how the work was done. A manager using output control sets a target, lets people choose their own method, and reads the number at the end: units shipped, revenue booked, defect rate, on-time delivery percentage.
The term is used in two settings, and they are easy to confuse:
- In organizational management, output control is one of three ways to control an organization, alongside behavioral control and clan control. This is the sense most of this article deals with.
- In production and operations, “input/output control” is a specific shop-floor technique for managing queues and lead times at a work center. It is covered in its own section below.
This article covers what output control is, how to run it, when it is the right choice and when it is not, its limits, and how it differs from behavioral and clan control. It also identifies bottlenecks that output measures alone will hide.
What is Output Control?
Output control is a control mechanism in which actual results are compared against planned results, and the gap between them drives corrective action. What is measured is the output of the work, not the work itself.
The distinction that matters is what a manager watches. Under output control, a sales manager sets a quarterly quota and reads the closed-deal figure. Under behavioral control, the same manager specifies the call script, the number of calls per day and the CRM fields to complete. Both are legitimate. They suit different situations, and the section on when to use output control sets out the conditions that decide between them.
Because it reads results after the fact, output control is a form of feedback control. It cannot stop the batch that has already been produced. It tells you the batch was wrong so the next one is not.
Some examples of output control include setting sales targets, tracking how many potential clients you reach in a specific time, and keeping an eye on the amount of unused ingredients left at the end of the week.
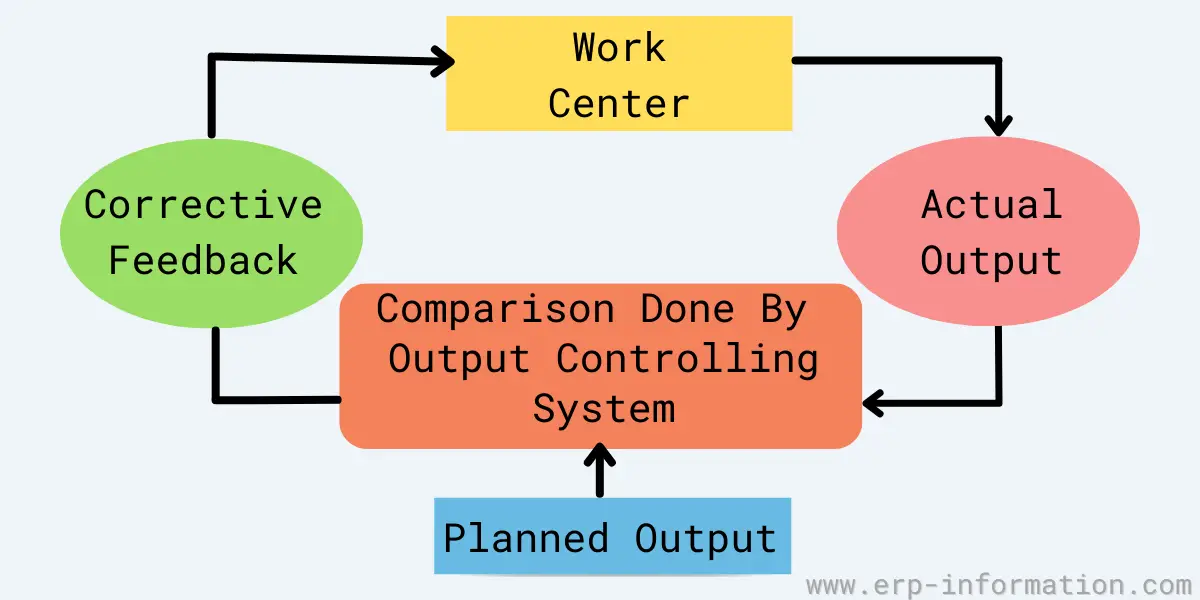
Input and Output Control in Manufacturing
In production planning the term appears as input/output control, and it means something more specific than the management concept above. It is a method of managing queues and work-in-process lead times by monitoring both the work flowing into a work center and the work flowing out of it.
Measuring output on its own tells you almost nothing. A work center producing 100 hours a week looks healthy until you notice it is being fed 120 hours a week. The queue in front of it grows by 20 hours every week, and the lead time for every order in that queue grows with it. This is why the technique tracks three pairs, not one:
- Planned versus actual input monitors the flow of work arriving. Input below plan means the work center is starved and will sit idle, whatever its capacity.
- Planned versus actual output monitors the performance of the work center itself. Output below plan points to a capacity problem: breakdowns, absence, scrap, tooling.
- Planned versus actual backlog (the queue) monitors lead time. This is the number that tells you whether the other two are in balance.
The queue is simply the difference between what went in and what came out, carried forward period by period:
Closing backlog = opening backlog + actual input − actual output
A worked example over four weeks, with an opening backlog of 40 standard hours and a plan of 100 hours in and 100 hours out each week:
| Week | Planned input | Actual input | Planned output | Actual output | Closing backlog |
|---|---|---|---|---|---|
| 1 | 100 | 105 | 100 | 95 | 50 |
| 2 | 100 | 110 | 100 | 92 | 68 |
| 3 | 100 | 102 | 100 | 96 | 74 |
| 4 | 100 | 108 | 100 | 94 | 88 |
Output is short by roughly 5 hours a week, which on its own looks like a minor capacity shortfall. The backlog column is the one that matters: it has more than doubled in a month. At an output rate of about 94 hours a week, an 88-hour queue means a new order waits close to a week before anyone starts it. Nothing on the shop floor is visibly broken, and the lead time has still nearly doubled.
The two corrective levers are different, and reading the wrong one is the usual mistake:
- Correct the output when the work center is failing to hit a plan it has the capacity to meet. Overtime, an extra shift, subcontracting, fixing the constraint.
- Correct the input when the plan itself is overloading the work center. This is done upstream by holding back order release, not on the shop floor. Releasing more work into a queue that is already growing does not produce more output, it only lengthens lead time and increases work in process.
ERP systems implement this directly. Infor LN, for example, reports actual against planned input, output and queue for each work center, plus a demonstrated load factor. The input side is normally governed further upstream by capacity planning, which is where a persistent imbalance should be resolved rather than absorbed as queue.
Features of Output Control System
- Output control is an active process
- It includes continuous evaluation of the products and services
- It is a follow-up action of the functional management
- It is a feedback process. The measurement happens after the output exists, which is what separates it from feedforward control
- It is corrective rather than preventive. It cannot stop the current output being wrong, only the next one
- Reduces losses, wastage, and deviation from standards
- Takes corrective actions based on feedback
Objectives of Output Control
- Ensure that the production process follows the predetermined standards to attain the desired output.
- To know the activities of the organization.
- To find out the corrective action with minimum effort, cost, and time.
- To synchronize efforts and mixed activities.
Steps to Keep Up the Standards of Output Product or Service

Here we are discussing five main steps to keep up the standards of your products or services. In short, you can call it the steps of the control process.
1. Formation of standards
This is the first step to maintaining the standards. It is the criteria against which the actual output is measured. Next, these standards review the desired result. These standards may be of two types.
- Quantitative standards: These standards are the standards that can be measured in terms of quantity, such as production and sales.
- Qualitative standards: These standards cannot be reduced to a number, such as employee motivation, industrial relations or service courtesy. They still have to be judged, which is exactly where output control is weakest.
2. Evaluation of performance
This step includes measuring performance concerning work in terms of control standards. Then, the evaluation becomes easy based on the established standards and goals.
If the evaluation finds any deviations, you can immediately take corrective actions.
3. Compare standard performance and actual performance
The third step is comparing actual performance with expected performance. This process gives you the deviations between standard and actual performance.
If the standards are quantitative, the comparison is arithmetic. Where the standard is qualitative, the deviation has to be established by keen observation and structured judgement, such as an appraisal rubric or a sampled quality audit, because there is no number to subtract.
4. Analysis of deviations
This fourth step is about the analysis of the deviation. You must thoroughly analyze the variation when the deviation exceeds the limit to determine the cause.
Then report to the manager or top management about the deviation’s cause and take the necessary action to correct it.
5. Take corrective actions
In this last step, the manager takes the required corrective procedures to reduce the deviation. For example, disciplinary actions will be the review of standards, employee training, and technical improvement.
Examples of Output Control
Example 1
On-time arrival rate is the standard output measure in commercial aviation, and it shows why the choice of measure matters as much as the target.
An airline that controls on this single number can improve it without improving anything a passenger would recognise. Padding the published block time makes the same flight arrive “early” without flying any faster. Boarding a delayed aircraft and holding it at the gate protects the departure metric. Both raise the score and neither raises punctuality.
This is the central lesson of output control and the reason it is paired with the limitations further down. The measure becomes the target, so it has to be chosen so that the only practical way to move it is to do the underlying work better. Airlines address it by controlling on a set of measures at once, such as on-time arrival, mishandled bags and involuntary denied boardings, so that gains bought by degrading one dimension show up in another.
Example 2
A company producing and selling electronics goods must ensure the standard of the products and longevity.
The finish must be high-end to attract the rich and funky and, at the same time, interest the ones after quality products.
One mobile phone company conducted a market survey after its brand value decreased.
It was found that despite starting at the top of the chart, mobile phones had fallen out of the competition.
It was found that while all its contemporaries had a massive battery capacity, this mobile phone had minimal capacity.
The company soon launched a newer version with upgraded features and huge battery capacity and took over the market.
Note what the control actually did here. It did not prevent the weak product from being launched, because the shortfall only became visible once sales and survey results existed. It shortened the time between the mistake and the correction, which is what feedback control is for.
Example 3
We can also take university test results as an example of output control. Test results and grades are reasonable output measures of students’ academic performance.
When the students do not perform well on the test, their results will not meet their desired results. At this point, they can take corrective actions by studying harder than earlier.
At some universities, students will be put on probation. If their grades are below the standard rate or their performance has not improved, they may not be promoted to further studies.
Output Control Advantages
Helps to achieve the objectives of the organization
The output control system controls and monitors the organization’s activities and ensures that all the activities are planned.
If it finds any variations in activities, immediately correct them and put the activities back on the planned path. This controlled process in the organization helps to achieve the objectives.
Uses the resources effectively
This technique monitors and ensures that all the activities are going according to the planned standards. Hence there is an effective use of resources.
Determines the precision of product standards
With the help of a control system, you can quickly determine the accuracy of the product standards. It also updates the criteria as per the environmental changes.
Motivates workers and subordinates
An effective control system shares the objectives and standards of appraisal with employees and subordinates.
It also helps them to overcome their problems. In this way, it motivates them to give their best.
Reduces the errors and maintains the quality of products
The output control system continuously monitors and corrects the errors that occur.
Managers immediately find the errors and take corrective actions to reduce the mistakes in the finished product or services.
Limitations of Output Control
Hard to set quantitative standards
Output control needs a number, and some of the most important work does not produce one. Research, legal advice, design and long-cycle relationship management all resist measurement on any timescale short enough to be useful for control. Where no credible output measure exists, forcing one produces a metric that is managed instead of the work.
The measure becomes the target
This is the characteristic failure of output control, and it follows directly from its main strength. Because people are told the result and left to choose the method, any method that moves the number is rational, including ones that damage the business. A call centre controlled on average handle time ends calls early. A sales team controlled on bookings discounts to close. A plant controlled on units produced builds what is easy rather than what is needed.
The usual mitigation is to control on a small set of measures that constrain each other, so that a gain bought by degrading an unmeasured dimension becomes visible somewhere else.
Uncontrollable external parameters
You will not be able to control external factors such as changes in technology, government rules and policies, and the customer’s taste.
Workers’ resistance
Resistance to output control is usually about the target rather than the monitoring. Where a quota is set without the people who have to meet it, is raised whenever it is met, or is applied to results that depend heavily on factors outside the individual’s control, it is experienced as arbitrary and gets gamed or resisted.
Continuous personal surveillance, such as CCTV or keystroke logging, is a common example of a control that provokes resistance, but it belongs to behavioral control, not output control. The two are frequently confused. Output control is indifferent to how someone spends the day and cares only about the result at the end of it.
Expensive
The control system requires a little more resources, time, and effort. Hence make sure that your expenses are giving your desired benefits.
Three Stages of Control

Control is classified by when it acts relative to the work. There are three stages, and output control is the third of them. It is not divided into the three.
| Stage | Name | When it acts | Example |
|---|---|---|---|
| Input | Feedforward (preventive) control | Before the work starts | Inspecting incoming material, screening and training staff before they take the job |
| Conversion | Concurrent control | While the work is happening | In-process gauging, a supervisor on the floor, statistical process control |
| Output | Feedback control | After the work is finished | Final inspection, sales against quota, customer complaints |
Output control sits in the third row. That placement is the whole point of it and explains both its advantages and its limits: it is cheap, it does not require you to understand how the work is done, and it is always too late for the unit being measured.
Feedback control is generally chosen where feedforward or concurrent control would cost too much or take too long, and where the process repeats often enough that correcting the next cycle is worth something. For a one-off, irreversible outcome it is close to useless, which is why safety-critical work is controlled at the first two stages instead.
Types of Organizational Control Systems

Apart from output control, Behavioral control, and Clan control are the other two.
Behavioral control gives attention to activities carried out by people. It controls the action that leads to the desired result.
Generally, different rules and procedures are used to set standards for behavioral control.
For example,
- You can see some signboards on the road while traveling, like don’t park the vehicles here, don’t overtake, etc. These are behavioral control systems.
- When you go to a restaurant or in the washroom of a company, you can see some instructions like “don’t wastewater.”
- In some industries, you can see no-smoking areas and switch-off mobile boards.
- Attendance of the students in class
- Punctuality of the students
All these are the best examples of behavioral control.
Clan control tells about values, traditions, and expectations to give their best to the organization. For example, dress codes in a company or a college campus.
Many organizations use all three types of control to get better output of products or services.
When to Use Output Control
Most explanations of output control stop at a list of advantages and disadvantages, which does not help you decide anything. The question a manager actually has is which of the three controls to use, and there is a well established answer to it.
William Ouchi set it out in A Conceptual Framework for the Design of Organizational Control Mechanisms (Management Science, Vol. 25, No. 9, 1979, pages 833 to 848). His argument starts from a simple observation: you can only monitor two things, the behavior of people or the output of that behavior. Which one is available decides the control you can use. Two conditions determine it.
- Knowledge of the transformation process. Do you understand how inputs become outputs well enough to write down the correct steps?
- Ability to measure outputs. Can you measure the result precisely, and soon enough to act on it?
| Knowledge of the transformation process: perfect | Knowledge of the transformation process: imperfect | |
|---|---|---|
| High ability to measure outputs | Behavior or output measurement Apollo program | Output measurement Women’s boutique |
| Low ability to measure outputs | Behavior measurement Tin can plant | Ritual and ceremony, clan control Research laboratory |
Ouchi’s own four examples explain the cells better than the labels do:
- Tin can plant. The technology is understood completely, so watching that the machines and operators follow the specified steps is enough to know that good cans are coming out the other end. Behavior control.
- High-fashion women’s boutique. Nobody can write the rules that make a buyer pick the right dresses. But markdowns, inventory turnover, sales volume and margin per buyer are all measurable with precision. This is the cell output control is made for.
- Apollo program. Every step of the transformation can be specified, and the output is unambiguous: the capsule gets there and back, or it does not. Both controls are available, so cost decides. Because the cost of a single failure is prohibitive, NASA chose elaborate behavior control with hundreds of ground controllers monitoring each step.
- Corporate research laboratory. There are no rules that reliably produce a breakthrough, and although a discovery’s value can eventually be measured, it may take decades. Neither control works, so the organization falls back on selecting people carefully and relying on shared professional values. Clan control.
The short version: use output control when you can measure the result well but cannot specify the method. If you can specify the method, behavior control is usually cheaper and catches problems earlier. If you can do neither, no amount of measurement will help and selection and culture have to carry the load.
The Apollo case is worth dwelling on, because it is the one managers get wrong. Having a good output measure does not mean you should control on it. When failure is irreversible or catastrophic, feedback arrives too late to be worth anything, and the more expensive control that acts earlier is the correct choice.
Related Management Practices
Three named practices come up constantly in discussions of organizational control. They are often lumped together as management fads, which obscures the more useful point: each one belongs to a different control type, and knowing which is which tells you what it can and cannot do.

1. Management by objectives (MBO): output control
Peter Drucker introduced management by objectives in The Practice of Management (1954). Manager and employee agree objectives together, individual goals are aligned with the organization’s, and performance is then measured against those agreed standards.
MBO is not a rival to output control, it is output control written down as a management system. It is the mechanism by which the target in an output control loop gets set, and the reason for agreeing it jointly rather than imposing it is that a quota someone helped set is far less likely to be gamed.
2. Quality circles: behavioral and clan control
A quality circle is a small group of workers doing similar work who volunteer to meet regularly and solve problems in their own area. The practice was developed in Japan in the early 1960s, associated with Kaoru Ishikawa and the Union of Japanese Scientists and Engineers, and it is an ancestor of modern continuous improvement.
The voluntary part is not incidental. A quality circle works on the method rather than the result, which puts it on the behavioral side, and it depends on shared commitment rather than on a target, which is clan control. A mandatory quality circle with a savings quota attached is neither, and generally does not work.
3. Sensitivity training groups (T-groups): clan control
T-groups are unstructured groups of roughly 8 to 15 people who meet to discuss their own reactions, feelings and beliefs about working together. They were widely used in organizational development from the 1960s and are far less common now.
They sit squarely in clan control. Nothing is measured and no method is prescribed. The intended effect is on shared understanding and values, which is precisely the mechanism organizations fall back on when neither behavior nor output can usefully be monitored.
FAQs
Why is output control important?
Output control is essential because it gives you a measurable result. You can determine the level of performance and monitor whether the business’s performance meets the expectation.
What are the three types of control systems in an organization?
Three types of control systems in an organization are
1. Output control
2. Behavioral control
3. Clan control.
What is the difference between output control and behavioral control?
Output control measures the result and leaves the method to the individual. Behavioral control specifies and monitors the method itself. Ouchi (1979) argued the choice depends on two conditions: use output control when you can measure results well but cannot specify how the work should be done, and behavioral control when you understand the process well enough to write down the correct steps.
Is output control the same as feedback control?
Yes. Control is classified by when it acts: feedforward acts before the work, concurrent control acts during it, and feedback control acts after the output exists. Output control is feedback control, which is why it can correct the next unit but never the one it just measured.
Conclusion
Output control means judging work by its results and leaving the method to the people doing it. It is cheap to run, it scales, and it does not require managers to understand every job they supervise. Those are real advantages and they are the reason it is so widely used.
Its two weaknesses follow from the same design. It is feedback control, so it always arrives after the output it measures, and it invites people to move the number by whatever means works. Ouchi’s test is the practical way to decide: control on outputs where you can measure results but cannot specify the method, control on behavior where you can specify the method, and where you can do neither, accept that selection and culture are doing the work instead.