DNC stands for direct numerical control, and today usually for distributed numerical control. Direct NC, from the late 1960s, had one central computer feed part programs block by block to several NC machine tools in place of punched tape. Distributed NC, the meaning ISO 2806 now uses, has a server store programs and send them to CNC machines.
DNC full form: Direct Numerical Control (the original 1960s meaning) or Distributed Numerical Control. ISO 2806:1994, which ISO reviewed and confirmed in 2023, defines DNC as distributed numerical control and calls direct numerical control “an obsolete term”.
Definition
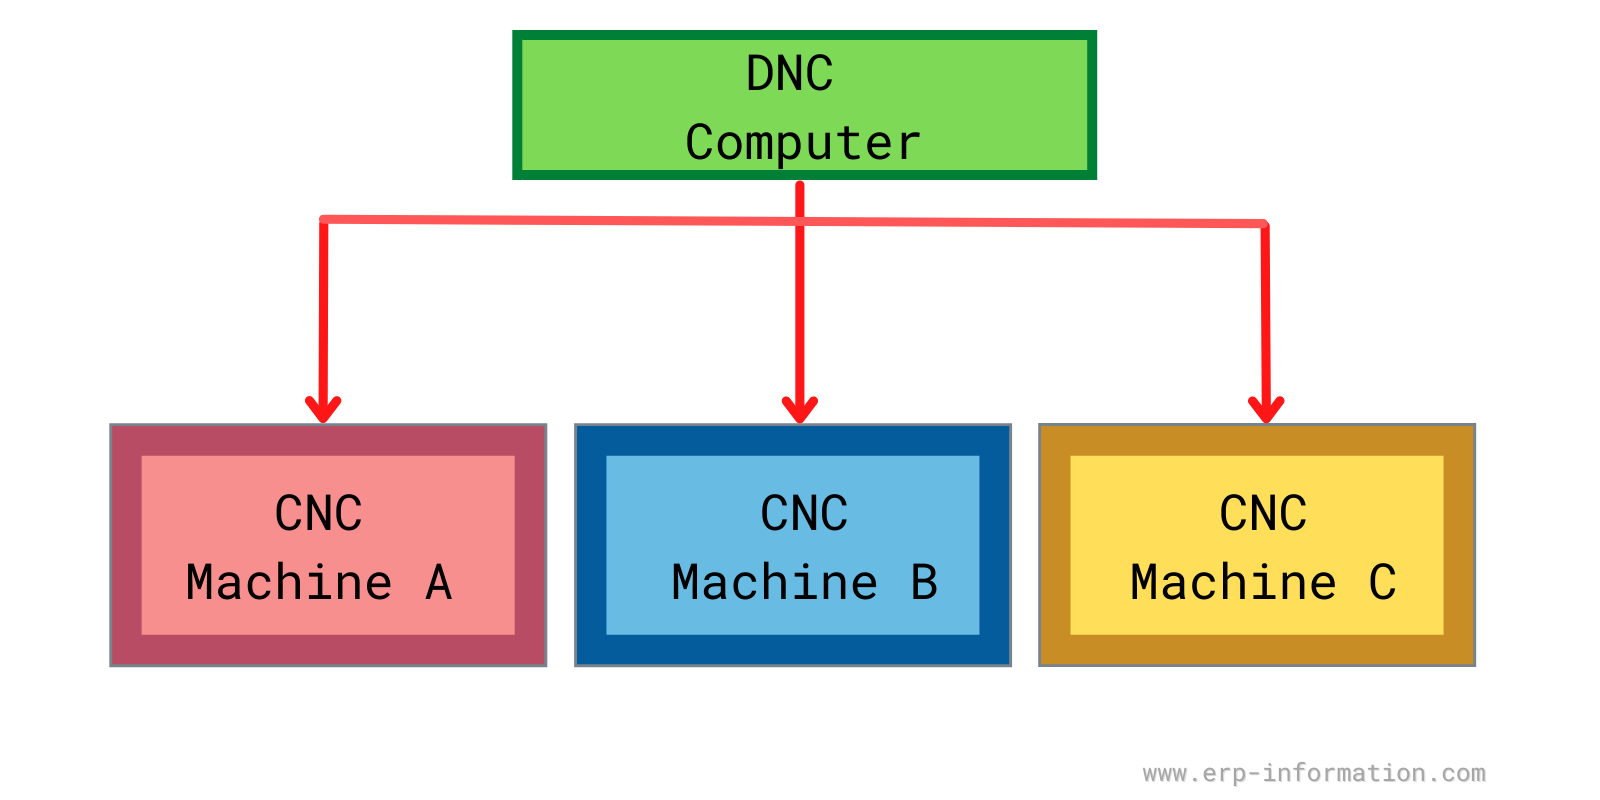
ISO 2806 defines distributed numerical control as a “hierarchical system for distributing data between a production management computer and NC” systems. The same standard defines numerical control (NC) as “automatic control of a process performed by a device that makes use of numeric data introduced while the operation is in progress”. Computerized numerical control (CNC) is the “realization of NC” using a computer to control the machine functions.
Direct NC and distributed NC are two different systems
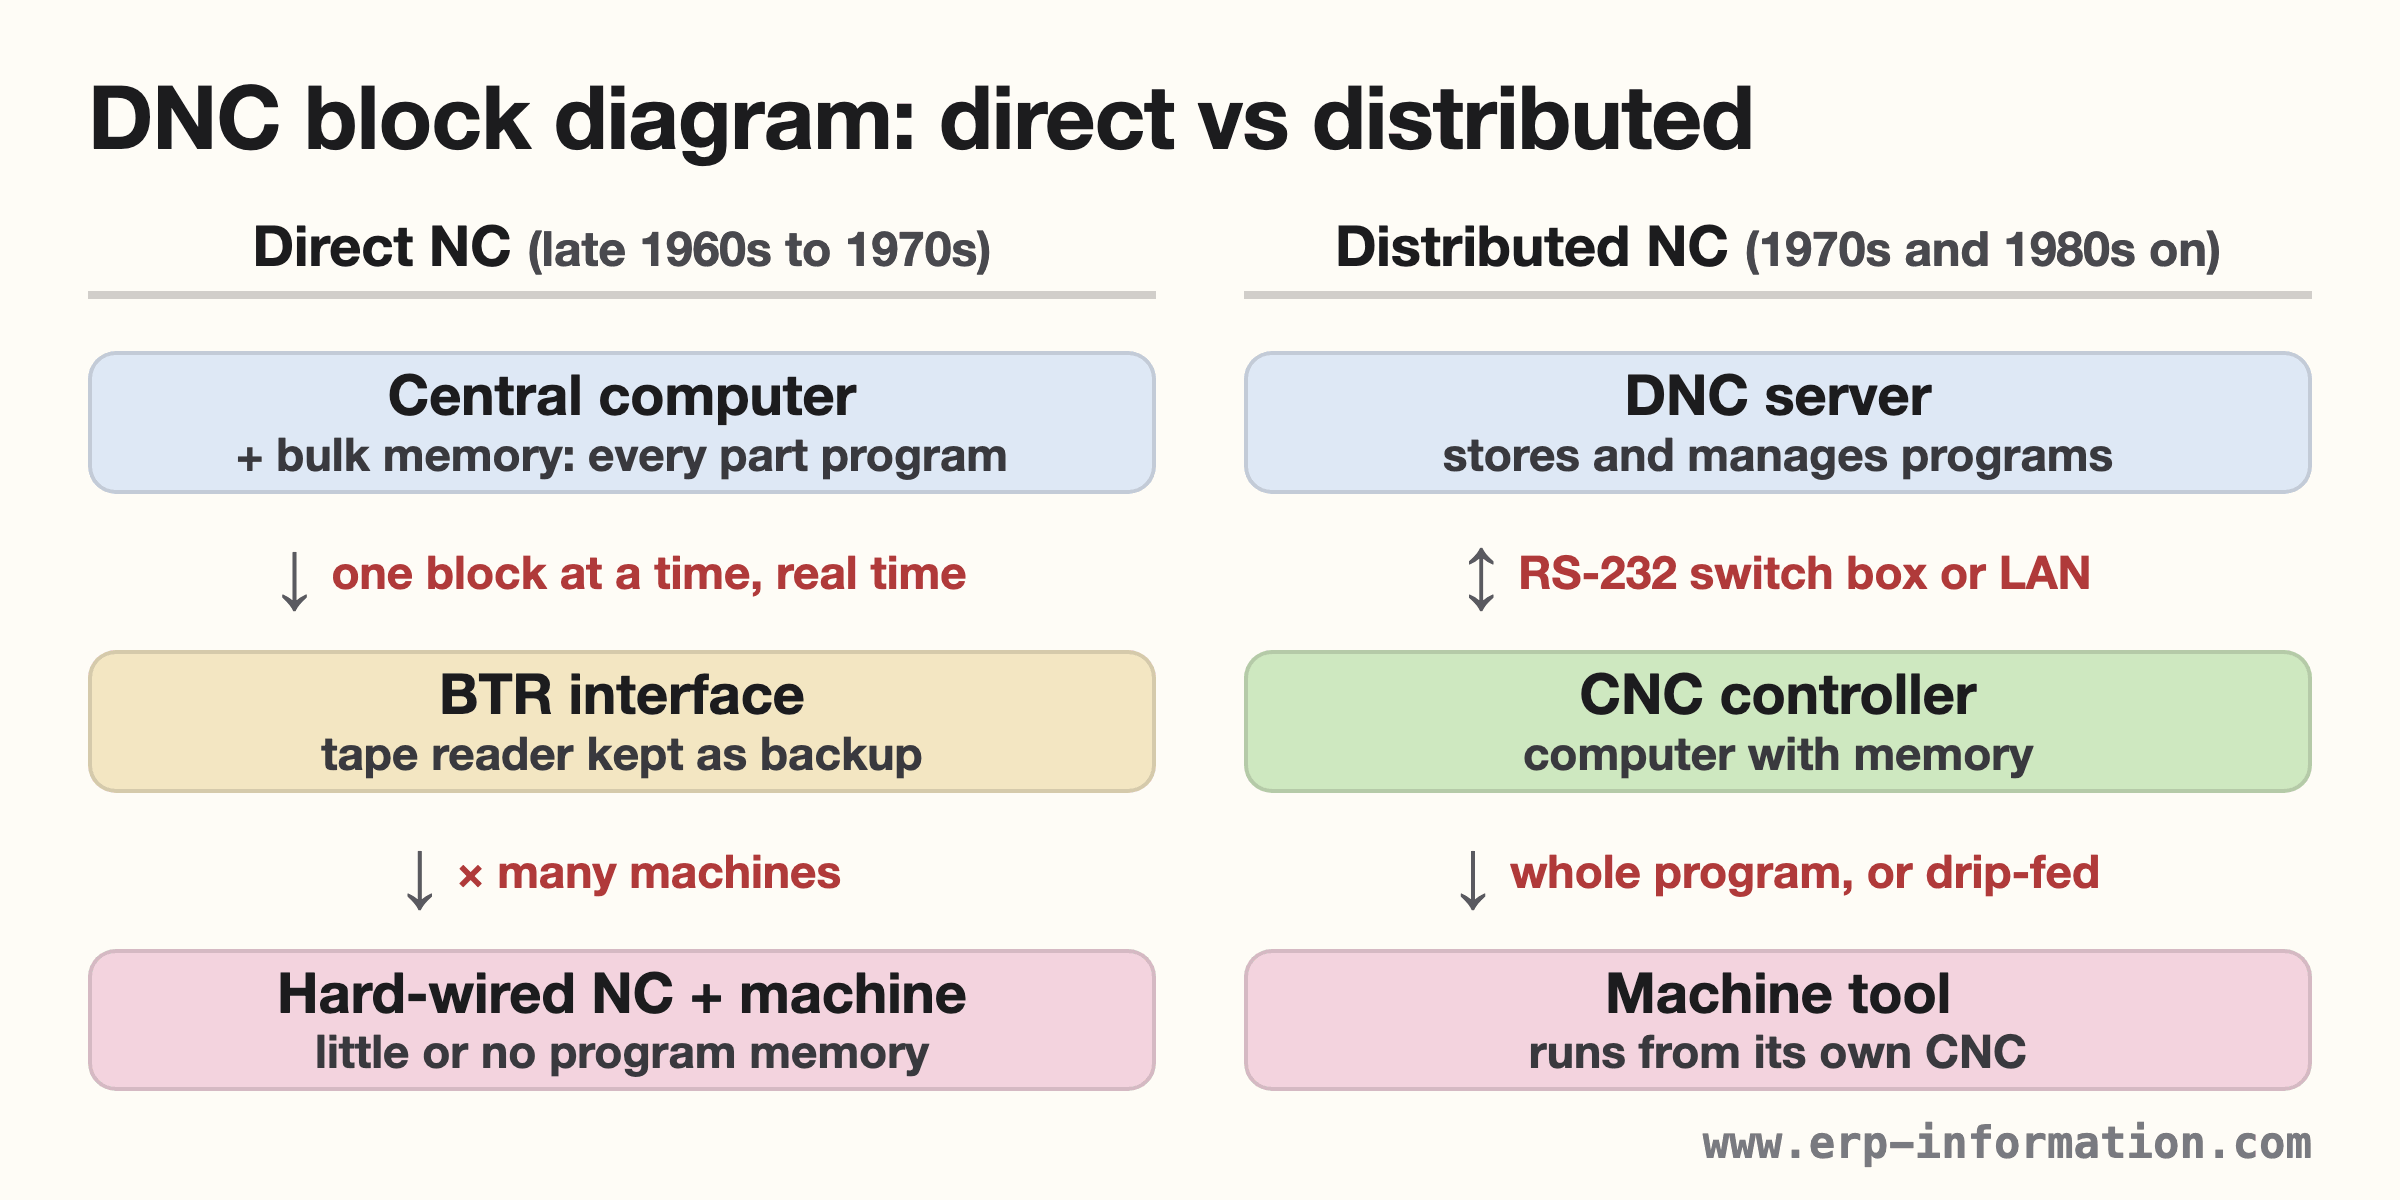
Direct numerical control came first. IIT Kharagpur’s NPTEL notes, which follow Groover’s textbook, call it “the first attempt to use a digital computer to drive the NC machine tool”, in the late 1960s before the advent of CNC. A single mainframe controlled a number of machine tools through direct connection and in real time. Instead of a punched tape, the computer sent the part program to each machine control unit (MCU) one block at a time, a mode called behind the tape reader (BTR). IGNOU dates the first systems to Cincinnati Milacron and General Electric in the mid 1960s; a Sundstrand patent for an on-line computer controlling machine tools was filed in October 1968.
Distributed numerical control followed as CNC machines spread in the 1970s and 1980s. Now each MCU is itself a computer, so the central computer sends complete part programs rather than one block at a time, and the CNC machines can run on their own. As East Tennessee State University’s course notes put it, “DNC can refer to either Direct N/C or Distributed N/C”.
| Point | Direct NC | Distributed NC |
|---|---|---|
| Era | Late 1960s to 1970s | 1970s and 1980s onward |
| Controller on the machine | Hard-wired NC with little or no program memory | CNC: a computer with its own memory |
| What the computer sends | One block at a time, in real time (BTR) | The whole program, or drip-fed in chunks |
| If the central computer fails | Every machine stops | Machines keep running programs already stored in them |
The tape reader did not disappear. Groover’s text notes that eliminating tape readers “was unrealistic”, because a backup way to load part programs was needed when the central computer was down.
What is computer numerical control (CNC)?
CNC is numerical control in which the machine control unit (MCU) is a dedicated computer rather than a hard-wired controller. ISO 2806 defines it as the realization of NC using a computer to control the machine functions. A CNC can store more than one part program and lets the operator edit programs at the machine tool.
DNC Machine
There is no single DNC machine. The term means a computer system that serves many machine tools. In Groover’s description of direct NC, the system had four components:
- Central computer, which called up each part program.
- Bulk memory at the central computer site, where all the part programs were kept.
- A set of controlled machines, each with its machine control unit.
- Telecommunication lines connecting the machines to the central computer.
What does a DNC machine contain?
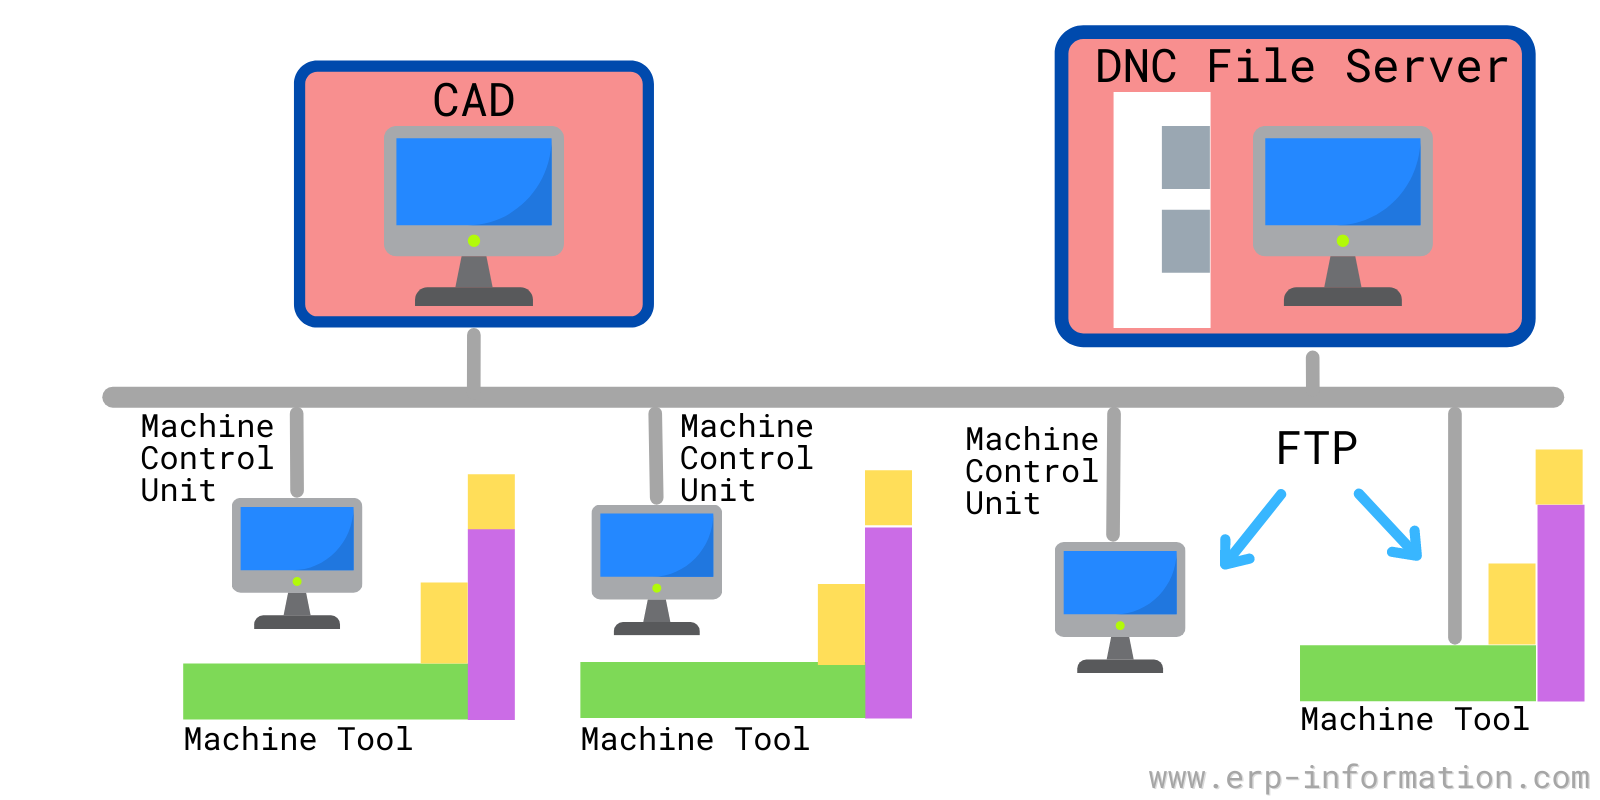
A DNC machine is really a DNC system. Groover’s original direct NC had four components: a central computer, bulk memory at the central computer site, a set of controlled machines, and telecommunication lines linking them. A distributed NC system has a DNC server that stores the programs, a network (an RS-232 switching box or a LAN), and CNC machines whose controllers hold the programs they run.
DNC is an extra cost on top of the CNC machines: IGNOU lists the network, the computer, terminals and the software. Its course unit says DNC pays off when many CNC machines are connected, when part programs are too large for the MCU’s memory, and when program variety is large and batch sizes are small.
The same unit gives a worked payback example: if DNC raises CNC operating efficiency by 2 to 5% and a 10-machine installation costs about Rs 500,000, the cost can be recovered in under a year. Treat those figures as the course’s illustration, not a current price.
Functions of Direct Numerical Control system
IGNOU groups the work of the DNC computer into three functions:
- Communications: downloading part programs to a CNC when it needs them, uploading programs that were edited at the machine, and drip feeding programs too large for the controller’s memory.
- Part program storage: one central library of programs for every connected machine.
- Ancillary functions: taking programs straight from the CAD/CAM or part programming system into the DNC computer’s storage, linking with shop floor control, and getting data from each MCU on the parts completed (part numbers and quantities).
A 1978 McDonnell Douglas patent draws the same line between DNC and CNC. The DNC computer “is used to disseminate manufacturing data to, and to collect data from, many MCU’s”. A CNC computer usually supports only one machine tool.
Advantages
- Removes the local tape reader as the routine way to load programs, which helps the entry of error-free programs.
- A large central store holds many part programs in one place.
- One neutral program (CLDATA) can be kept and post-processed for each machine when it is downloaded, instead of storing a separate version for every machine.
- Programs edited at the machine can be uploaded back, so the library stays current.
- Distributed NC lets CNC machines go into service first and DNC be added later, and redundant computers make it more reliable than the original direct NC.
Disadvantages
- Direct NC: when the central computer was down, every machine was down, because no machine held its own program.
- Cost: the network, computer, terminals and software come on top of the machines.
- Groover’s text adds that some claimed advantages proved overly optimistic, and the high investment deterred a conservative industry.
Types of direct numerical control
There is no single list of DNC types. Textbooks and syllabi classify DNC in three different ways, so check which one your course uses:
| Classified by | Types | Where it comes from |
|---|---|---|
| How direct NC fed the machine | Behind the tape reader (BTR) system; specialized MCU | Indian polytechnic notes (Government Polytechnic Panchkula) |
| How distributed NC is wired | Switching network; local area network (LAN) | Groover, as taught in IIT Kharagpur’s NPTEL course |
| How programs travel today | Serial (RS-232) or network (Ethernet); whole download or drip feed | IGNOU and DNC software makers |
In a BTR system the computer connects to the regular NC controller, which uses two buffers: one receives the next block while the other drives the machine. Its cost is very low. A specialized MCU replaces the normal controller with one built to communicate with the computer, and achieves a better balance between interpolation accuracy and metal removal rate than BTR. IGNOU also uses BTR for retrofits: older NC and CNC controllers with little or no memory get a special interface unit plugged into the tape reader port.
In a switching network, a data switching box connects the central computer to one CNC machine at a time over RS-232-C. That limits how many machines the system can serve; an RS-232-C multiplexer raises the number. A LAN, used for DNC since the early 1980s, can be organized as a hierarchy in which a host computer coordinates satellite computers, each responsible for a number of CNC machines.
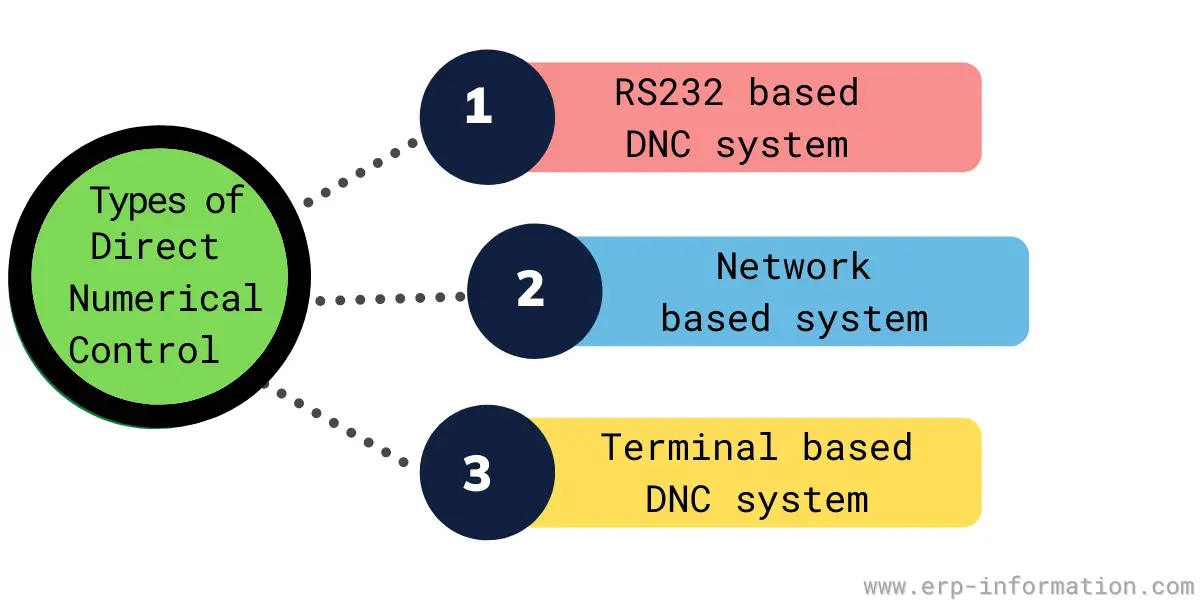
RS232 – based
IGNOU describes the usual DNC link as a PC’s RS-232C serial port wired to the CNC, at baud rates from 110 up to 19,200. RS-232-C originally limited the cable to 15 metres; later revisions specify a 2,500 pF load instead, about 15 to 20 metres depending on the cable. The standard’s maximum data rate is 20 kbit/s. Stand-alone USB DNC boxes now drip-feed straight from a USB stick over RS-232C, replacing the PC.
Terminal-based
The older diagram above, from an earlier version of this page, lists a terminal-based type. None of the textbooks, syllabi, standards or other guides we read uses it. The closest real feature is remote request: the operator calls a program from the machine’s own control, which DNC software such as NCnet and DNC-Max supports.
Network-based
Newer controls connect over Ethernet. Programs move by FTP, or by a control maker’s own protocol: DNC-Max, for example, supports HEIDENHAIN LSV-2 over TCP/IP and FANUC FOCAS. Older serial-only machines can join the network through serial device servers. (An earlier version of this page named a “TCP/IP Direct Control Protocol (DCP)”; we found no such DNC protocol. The industrial protocol abbreviated DCP is PROFINET’s Discovery and Basic Configuration Protocol, used for device setup, not program transfer.)
Drip feeding: when the program is bigger than the control’s memory
Drip feeding sends a program in pieces while the machine runs it. CNCCookbook’s description: the g-codes “come to the machine a few at a time when the machine is ready to execute them”. ETSU’s notes explain why it exists: complex mold programs can exceed ten megabytes, too large for the memories of older CNC machines.
The line speed matters. Assume the common serial framing of one start bit, eight data bits and one stop bit, so ten bits per character. Then a 10 MB program takes about 2.9 hours just to transmit at 9,600 baud, and about 1.4 hours at 19,200 baud (our calculation). The link has to stay up for the whole cut, and DNC software such as CIMCO DNC-Max offers a DNC restart function.
Direct Numerical Control Software
DNC software is the program on the server side: it stores the part programs, sends them to each machine, and receives them back. These are products whose makers describe them as DNC or program-transfer tools, checked on each maker’s own site on 11 October 2026:
| Product (maker) | What it does | Connects over |
|---|---|---|
| NCnet (CADEM Technologies, Bengaluru) | Program transfer and drip feed; full version for unlimited machines, free NCnet Lite for one machine | RS-232 port on the machine; LAN or Wi-Fi only through serial converters |
| Antech DNC (Antech Micro Systems, Pune) | Program management for up to 50 CNC machines per licence; also tape-reader and floppy emulators for old machines | RS-232, Ethernet, wireless and USB |
| DNC-Max (CIMCO, Denmark) | Central send, receive and drip feed for CNCs, robots and PLCs; up to 4,000 ports per server | Serial device servers, Ethernet FTP, HEIDENHAIN LSV-2, FANUC FOCAS |
| Predator DNC (Predator Software, Oregon, USA) | Transfers programs, offsets and parameters; up to 4,096 machines per PC or server | 50+ protocols over parallel, RS-232, RS-422 and Ethernet |
| Program Transfer Tool (FANUC) | Moves programs between a PC and up to 255 FANUC controls, including to data server storage | The control’s embedded Ethernet |
| TNCremo (HEIDENHAIN) | Free PC package for file transfer between a PC and a TNC control | PC to control link |
Two notes. CIMCO is still its own company: Sandvik’s March 2025 deal covered only CIMCO’s “probing and post processor business lines”. And FANUC’s FOCAS2 is a developer library for Windows applications that read and write CNC data over Ethernet or HSSB. It is not a DNC package by itself; DNC products such as DNC-Max use it to talk to FANUC controls.
Some names you will see on Indian supplier lists are resellers rather than makers. Niha Solutions (Bengaluru) lists CIMCO DNC-Max among the brands it sells, and Technovision CNC (Pune) trades USB and wireless DNC boxes that drip-feed a program from a USB stick over RS-232C, replacing the PC. Next Tech CNC (New Delhi) sells and services CNC machines but lists no DNC product, and we could not find a CNC business trading as Skytrends.
Uses of Direct Numerical Control Software
Read across the makers’ own descriptions, DNC software does six jobs:
- One program library: “Stores and organizes all NC programs in one secure location”, in the words of Predator’s US distributor.
- Send and receive: download programs to the control and upload edited ones back.
- Drip feed: stream programs too large for the control’s memory; CIMCO notes unlimited file size works only “if supported by CNC”.
- Remote request: the operator calls a program from the control itself; CIMCO also allows a mobile device or a barcode reader.
- More than programs: Predator DNC also moves CNC variables, offsets, parameters and PLC registers.
- Revision control and backup: Siemens describes NC program management with versioning, direct transfer to the machine and automatic data backup, used on all 107 machine tools at its Bad Neustadt factory.
Machine monitoring is usually a separate product: CIMCO sells MDC-Max and Predator sells Predator MDC for data collection and OEE.
Differences between Direct Numerical Control and Computer Numerical Control
NC, CNC and DNC side by side:
| Point | NC | CNC | DNC |
|---|---|---|---|
| Control | Hard-wired, run from punched tape or cards | A dedicated computer that stores the program | A remote computer holding programs for many machines |
| Machines per computer | No computer | Usually one | Many |
| Where the computer sits | No computer | On the shop floor | Usually away from the machines |
CNC also allows editing of programs at the machine tool, and a DNC computer receives those edited programs back (uploading). Two points are often mixed up. DNC does not replace the CNC: IGNOU notes that each machine is still “controlled by its MCU” while it communicates with the DNC computer. And only the original direct NC stopped every machine when the central computer failed; distributed NC machines keep running programs already stored in them.
Where DNC is heading: MTConnect and OPC UA
DNC moves programs to the machines. Two newer standards cover the other direction, data from the machines. MTConnect (ANSI/MTC1.4-2018) is a vocabulary that lets any application read data from compliant machines. It was first released in late 2008 and is maintained by the not-for-profit MTConnect Institute, which says all agent communication is “read-only HTTP”.
OPC UA for Machine Tools (OPC 40501-1, version 1.02.0, published 1 November 2024) models a machine tool for monitoring and job overviews, for exchange with MES, SCADA, ERP and analytics systems. The umati initiative builds on it. It is not purely read-only: the model includes an optional file system and a “Remote” mode in which “the machine tool can receive CNC files via a remote access mechanism”.
FAQs
What is the full form of DNC?
DNC stands for Direct Numerical Control, the original late 1960s system in which one computer fed several NC machines in real time. Today it usually stands for Distributed Numerical Control: ISO 2806 defines DNC this way and calls direct numerical control an obsolete term.
What are the key components of a DNC system?
Groover lists four for direct NC: a central computer, bulk memory at the central computer site, the set of controlled machines, and telecommunication lines. A distributed NC system has a DNC server with DNC software, a network (an RS-232 switching box or a LAN), and CNC machines whose own controllers run the programs.
What is drip feeding in DNC?
Drip feeding sends a part program to the CNC in small pieces while the machine runs it, so a program larger than the control’s memory can still be machined. The connection has to stay up for the whole cut, and DNC software such as CIMCO DNC-Max offers a restart function.
Key points to remember
- DNC has two meanings: direct NC (late 1960s, block by block in real time) and distributed NC (whole programs to CNCs, the ISO 2806 meaning).
- Direct NC: central computer, bulk memory, telecommunication lines, controlled machines. If the computer failed, every machine stopped.
- Distributed NC: a server stores programs and sends them to CNCs over an RS-232 switching network or a LAN; each machine runs on its own.
- Types depend on the scheme: BTR or specialized MCU; switching network or LAN; serial or Ethernet.
- Drip feed streams programs too large for the control’s memory, and the link must stay up for the whole cut.
- MTConnect reads machine data; OPC UA for Machine Tools adds monitoring, job overviews and an optional route for CNC files.
You will also like:
- What is a Computerized Maintenance Management System?
- What is Application Programming Interface (API)?
- What is Database Management System (DBMS)?
- What is Online Analytical Processing (OLAP)?
- What is Data Warehouse? Details, benefits, and tools
How we researched this page
Updated 11 October 2026. We read ISO 2806 on ISO’s own platform, IIT Kharagpur’s NPTEL notes, two IGNOU units, university and polytechnic course notes, two DNC patents from 1968 and 1978, the MTConnect, OPC Foundation and NIST documents, and each DNC software maker’s own pages. We also checked every company our earlier version listed as a DNC software vendor, and removed a protocol name (“Direct Control Protocol”) that no source supports. The drip-feed transfer times are our own calculation, with the assumption stated. The block diagram is new and drawn from the components these sources name.
References
- ISO 2806:1994 Industrial automation systems, Numerical control of machines, Vocabulary (terms 2.1.1 to 2.1.3)
- ISO catalogue: ISO 2806:1994, reviewed and confirmed 2023
- IIT Kharagpur NPTEL course 110105155, lecture notes (weeks 4 and 5, after Groover)
- IGNOU BME-004 Unit 7: Direct Numerical Control
- IGNOU BME-005 Unit 5: CNC Machines
- East Tennessee State University, ENTC 3710: DNC notes
- Government Polytechnic Panchkula: CNC e-content (types of DNC)
- Landmark University MCE527, NC programming lecture 9
- Groover, Automation, Production Systems and CIM: Direct Numerical Control (reproduction on BrainKart)
- US patent 3,668,653 (Sundstrand, filed 1968)
- US patent 4,281,379 (McDonnell Douglas, filed 1978)
- Texas Instruments SLLA037A: Interface circuits for TIA/EIA-232-F
- MTConnect Institute
- NIST AMS 200-2: Smart Manufacturing Systems Test Bed (MTConnect)
- OPC Foundation: OPC 40501-1 OPC UA for Machine Tools, v1.02
- umati: about
- CNCCookbook: DNC software, drip feed
- CADEM: NCnet DNC software
- CADEM: What is DNC software
- CADEM NCnet Lite listing (IndiaMART)
- Antech Micro Systems: DNC software and systems
- Antech Micro Systems: Who we are
- CIMCO: DNC-Max
- CIMCO DNC-Max v8 help: network protocol settings
- Sandvik press release, 3 March 2025: CIMCO business lines acquired
- Predator Software: Predator DNC
- Shop Floor Automations: Predator DNC
- FANUC America: Program Transfer Tool
- FANUC America: FOCAS2 Library
- HEIDENHAIN: TNCremo (Infobase 340447-04)
- Siemens reference: NC program management, Bad Neustadt
- Niha Solutions: brands
- Technovision CNC: USB DNC (IndiaMART)
- Next Tech CNC: products (IndiaMART)
Using Google Search? Add erp-information.com as a preferred source.